Blog
How to Choose an EPS Casting Pattern Mould?
Choosing an Eps Casting Pattern Mould is a technical decision, not merely a price comparison. The mould shapes foam beads, controls expansion, and influences every later casting stage. A small mismatch at the parting line can create flashing, uneven walls, or costly trimming. The right choice begins with the component’s geometry, production volume, required tolerance, and alloy temperature.
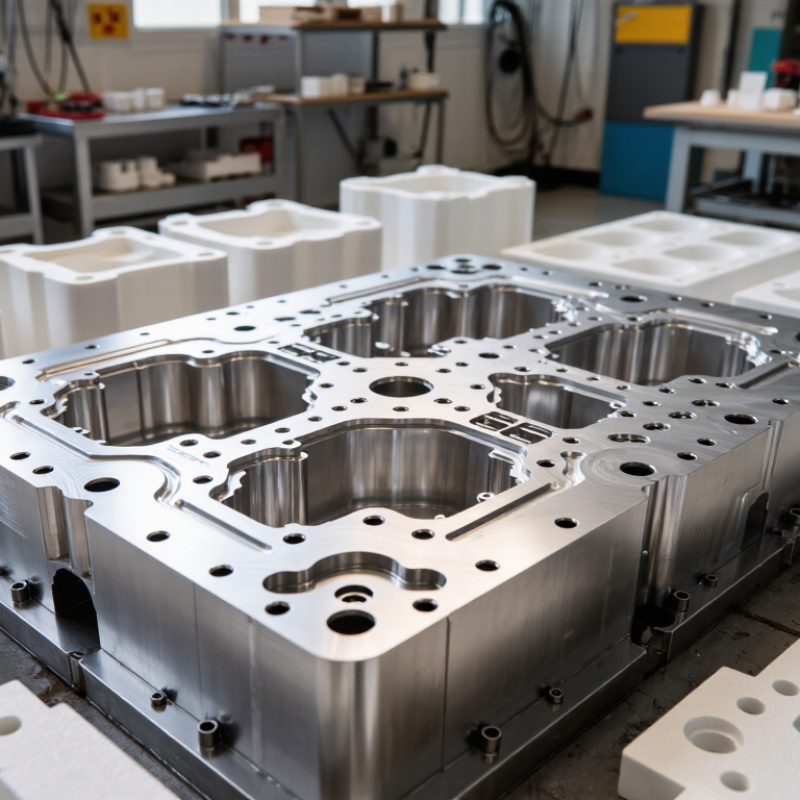
John Campbell, a widely recognized authority on casting technology, states, “The quality of a casting is determined by the quality of the liquid metal entering the mould.” His principle also applies to lost-foam production. A reliable Eps Casting Pattern Mould should support stable bead filling, consistent steam heating, adequate venting, and easy pattern release. Aluminium tooling may suit many production runs, while reinforced resin tooling can offer a practical option for prototypes or limited quantities. The decision depends on cycle demands.
Look closely at the details. Check cooling channels, ejector access, coating compatibility, and dimensional records. Ask whether the supplier has produced similar shapes, such as deep ribs, narrow cores, or uneven wall sections. Request trial samples.
Do not trust polished promises alone.
A mould may look precise yet perform poorly after repeated heating cycles. Suppliers should explain their inspection methods and correction process. Some choices remain uncertain, especially when the design contains thin sections or complex internal cavities. That uncertainty deserves testing, not optimism. A careful selection process combines engineering data, operator experience, and honest review of early defects. It may take longer initially, but it reduces avoidable rework and improves casting consistency.
Define the casting target: alloy, part size, and 20–30 kg/m³ EPS density
How to Choose an EPS Casting Pattern Mould?
Define the casting target before designing the EPS pattern mould. Identify the alloy, part size, wall thickness, and expected production volume. Aluminium, iron, and steel require different thermal considerations.
Their pouring temperatures can range from about 660°C to above 1,500°C. The mould must therefore support suitable filling, venting, and dimensional control. American Foundry Society process guidance also stresses that alloy selection influences gating, shrinkage, and surface quality.
Part size matters more than many designers expect. A large pattern can distort during handling, coating, or drying. Thin ribs may collapse. Heavy sections may need stronger supports or segmented mould construction.
For most lost-foam applications, an EPS density of 20–30 kg/m³ provides a practical starting range. Lower density improves foam decomposition but may reduce handling strength. Higher density feels safer, yet it can increase gas generation and casting defects.
Measure density under a recognized method, such as ISO 845:2018, rather than trusting supplier labels. Check actual mass and volume from trial samples. This step is often skipped. It should not be.
The right mould also maintains consistent bead fusion, accurate shrinkage allowance, and clean pattern release. Data from the European Foundry Association’s industry reports shows that process efficiency and defect reduction remain major foundry priorities.
Still, density alone cannot solve poor venting or unsuitable alloy temperatures. Testing one small section first is wiser than committing to a full-size mould.
Set pattern accuracy: include 0.5–1.0% dimensional shrinkage allowance
Choosing an EPS casting pattern mould begins with dimensional control. Set a 0.5–1.0% shrinkage allowance for the pattern, especially when casting aluminium or iron components. This range reflects common lost-foam practice, but it is not universal. ASM Handbook, Volume 15, explains that alloy contraction depends on composition, pouring temperature, and section thickness. A 500 mm housing may therefore require 2.5–5 mm of added length.
Pattern accuracy also depends on EPS density and bead fusion. Low-density foam can distort around thin ribs or deep corners. A moulding workshop should verify density, steam pressure, and cooling time for every production batch. ISO 8062-3 provides casting tolerance guidance, while industry lost-foam studies commonly report dimensional variation near 0.5–1.0% when process conditions remain stable. Measurement matters. Check the finished pattern with a calibrated gauge, not visual judgment.
Do not apply one allowance blindly. A thick base may contract differently from a narrow wall. Complex patterns need local compensation, draft review, and trial sampling. I have found that an initial 0.8% setting is practical, but it still needs correction after the first castings. Temperature records, pattern measurements, and casting inspection should be compared together. Small errors accumulate. A 1 mm mismatch at one joint can become a visible assembly problem. Avaliable data can guide the mould choice, but real process evidence should make the final decision.
How to Choose an EPS Casting Pattern Mould?
Set pattern accuracy by applying a 0.5–1.0% dimensional shrinkage allowance to the nominal casting size.
The chart shows the calculated EPS pattern dimensions for nominal casting sizes of 100 mm, 250 mm, and 500 mm. A 0.5% allowance adds 0.5 mm, 1.25 mm, and 2.5 mm respectively, while a 1.0% allowance adds 1 mm, 2.5 mm, and 5 mm. Select the allowance according to the casting process, material behavior, mould accuracy, and dimensional validation requirements.
Compare mould materials by heat transfer and production-cycle requirements
How to Choose an EPS Casting Pattern Mould?
Mould material directly affects heat transfer and production-cycle stability. Aluminum usually transfers steam and cooling energy quickly. This helps EPS beads expand, fuse, and cool with fewer uneven areas. In practical trials, a well-designed aluminum mould can shorten cycle times noticeably. Heat moves quickly. However, aluminum may cost more and can suffer from dents or distortion without careful handling.
Epoxy moulds can suit prototypes and smaller production runs. They are easier to modify, but their lower thermal conductivity may extend steaming and cooling periods. Steel provides strength for repeated production, although it often needs effective internal channels. Without proper channel design, its durability cannot compensate for slower heat movement. That assumption can fail. Experienced engineers should compare actual mould temperature readings, not rely only on material tables.
Tips: Record steam pressure, cooling time, demoulding temperature, and surface defects during trials. Check the thickest pattern section first. It often controls the entire cycle. Leave access for cleaning blocked vents and inspecting seals. A small venting mistake can create visible bead marks. We once underestimated cooling time on a dense pattern, so the next design included more cooling passages and a longer stabilization check. Results improved, but not perfectly. Review the data after every batch.
How to Choose an EPS Casting Pattern Mould? - Compare Mould Materials by Heat Transfer and Production-Cycle Requirements
| Mould Material | Typical Thermal Conductivity (W/m·K) | Heat-Transfer Behaviour | Typical EPS Production-Cycle Suitability | Dimensional Stability | Durability and Maintenance | Best-Fit Production Requirement | Main Limitations |
|---|---|---|---|---|---|---|---|
| Aluminium Alloy | Approximately 120–200 | High thermal conductivity promotes rapid and relatively uniform steam heating, bead fusion, and cooling. It also supports efficient heat removal when cooling channels or water circuits are integrated. | Excellent for short and repeatable cycles | Good when the mould is properly designed and supported; thermal expansion must be considered for tight tolerances. | Good wear resistance and easy machining. Surfaces may require protection against abrasion, corrosion, or damaged vents. | Medium- to high-volume EPS production, frequent tool changes, and applications where cycle time is a major cost factor. | Higher material and machining cost than resin tooling; soft surfaces can be marked by improper handling or abrasive contamination. |
| Steel | Approximately 15–50 | Lower conductivity transfers heat more slowly than aluminium. Thick sections may develop longer heating and cooling gradients unless the mould includes effective thermal management. | Suitable for long runs when cycle time is less critical | Very good stiffness and dimensional retention, especially for large or heavily supported moulds. | Very high mechanical durability and wear resistance. Heavier to handle and may need corrosion protection, drainage, and careful vent maintenance. | High-wear applications, large moulds requiring high rigidity, or production where tool life is more important than the shortest cycle. | Greater weight, slower heat response, higher handling loads, and potentially longer cycles without optimized channels and venting. |
| Epoxy or Filled-Resin Tooling | Approximately 0.2–1.5 | Low conductivity creates a thermal barrier. Heating and cooling are comparatively slow, and local hot or cold spots are more likely in thick tooling sections. | Best for prototypes, samples, and low-volume production | Good initially, but dimensional change can occur with temperature, moisture, ageing, or repeated thermal cycling. | Fast to produce and relatively economical for complex shapes. More vulnerable to impact, abrasion, steam exposure, and repeated demoulding than metal tooling. | Prototype validation, short product runs, bridge tooling, and applications where low initial tooling cost is more important than cycle speed. | Limited service life under intensive steam cycles; difficult repairs, lower heat-transfer performance, and greater risk of surface degradation. |
| Silicone Rubber | Approximately 0.15–0.30 | Very low conductivity and elastic walls provide limited heat-transfer efficiency. It is not normally selected for fast, high-throughput EPS bead moulding. | Generally limited to prototypes or specialised low-volume forms | Flexible rather than rigid; suitable for undercuts and release-friendly geometries, but not for applications requiring high dimensional repeatability under pressure. | Easy release and useful for complex details. Susceptible to tearing, compression set, surface damage, and shortened life under repeated heat and mechanical loading. | Complex prototype shapes, limited sample quantities, and moulds where flexibility or easy part release is essential. | Low stiffness, slow thermal response, limited pressure resistance, and poor suitability for demanding production cycles. |
| Composite Tooling with a Metal Heat-Transfer Skin | Depends on construction; commonly approximately 1–20 overall | A thin metal working surface can improve local heat transfer, while the composite backing reduces weight. Performance depends strongly on skin thickness, bonding, insulation, and channel layout. | Suitable for medium-volume production when weight reduction is valuable | Good when the backing structure controls distortion and the metal skin is adequately supported. | Lower weight than a solid metal mould and adaptable to large tools. Bond lines, inserts, and thermal fatigue require inspection. | Large or complex moulds requiring a balance between weight, cost, rigidity, and moderate cycle performance. | More complex design and repair; uneven construction can create thermal gradients or local distortion. |
Select venting, filling, and ejection features for foam bead expansion
How to Choose an EPS Casting Pattern Mould?
An EPS pattern mould must manage venting, filling, and ejection as one system. EPS beads contain approximately 98% air, according to technical guidance from the EPS Industry Alliance. Steam therefore needs a clear route through the bead pack. Use distributed vents near corners, ribs, and deep pockets. Blocked vents can leave shiny surfaces, weak welds, or trapped moisture. Small details matter.
Filling should match bead size, pre-expansion density, and cavity geometry. Place multiple fill ports when the pattern is wide or irregular. Balanced filling reduces density variation between the centre and edges. Plastics—The Facts 2023 reports 400.3 million tonnes of global plastics production in 2022. That scale increases pressure for repeatable, low-waste tooling. However, production volume does not excuse poor mould design. A short test run is still necessary.
Ejection needs gentle force. Use broad stripper surfaces or air assistance instead of narrow pins near fragile details. Add draft to vertical walls, but avoid excessive draft on tight dimensional features. I have found that vent locations often need adjustment after the first trial. The drawing may look correct. The foam disagrees. Record fill time, steam pressure, cooling time, and release damage during testing. These observations provide stronger evidence than visual inspection alone. A reliable mould is not merely fast; it releases a stable pattern without crushing bead structure.
Verify mould performance through trials, tolerance checks, and defect data
How to Choose an EPS Casting Pattern Mould?
A mould should prove its value during production trials, not only through drawings. Request a trial with the actual EPS grade, bead size, and steam conditions. Watch filling around thin ribs, deep pockets, and sharp corners. These areas expose weak venting quickly. Record cycle time, steam pressure, cooling time, and ejection force for every shot.
Tolerance checks need measured evidence. Use a calibrated CMM, height gauge, or suitable inspection fixture. Measure critical lengths, wall thickness, hole positions, and parting-line mismatch. Compare at least 30 patterns when possible. A single good sample can hide unstable shrinkage. For many castings, a practical starting point is ±0.3 mm on key features, but the drawing and process must decide the final limit.
Defect data is more useful than visual opinions. Photograph dents, incomplete fusion, burn marks, and sticking after each trial. Link every defect to a cavity, vent, insert, or process setting.
I once accepted a mould after five clean shots. Later, repeated cycling revealed uneven cooling near one corner. That mistake changed my inspection routine.
No trial is perfect. Leave room for doubt. Choose the mould with stable results, accessible maintenance points, and records that another engineer can verify.

